SLS 3D printing (selective laser sintering) uses a laser to fuse polymer powder into strong, functional parts with no support structures. It handles complex geometry and large parts in one piece, and it is a proven choice for prototypes, fixtures, and low-volume production parts. Our shop is in Coopersville, Michigan, just west of Grand Rapids, and we ship parts nationwide.
How SLS 3D Printing Works
Selective laser sintering was developed and patented by Dr. Carl Deckard and Dr. Joe Beaman at the University of Texas at Austin in the mid-1980s. Their startup, DTM, built the first SLS machines and was acquired by 3D Systems in 2001.

- The build platform lowers by one layer, 0.004″ to 0.006″ depending on the material.
- A recoater spreads a fresh layer of heated powder across the build area.
- A laser traces each part’s cross-section, sintering the powder into solid plastic.
- The process repeats layer by layer. Unsintered powder surrounds and supports the parts, so no support structures are needed.
- The finished build cools slowly, usually about as long as it took to print. The parts are then removed from the powder and cleaned by hand, with air jets, and by bead blasting.
Because parts are supported by the surrounding powder, SLS can build overhangs, interlocking parts, and internal channels that would be difficult or impossible with other processes.
When to Choose SLS 3D Printing
SLS makes tough, functional parts with good accuracy, high strength and stiffness, good chemical resistance, and the ability to handle elevated temperatures. Choose SLS for:
- Functional prototypes that need to perform like production parts
- Low-volume production parts, often as a replacement for injection-molded nylon
- Larger nylon parts that need to be printed in one piece
- Complex geometry, including internal channels, conformal cooling lines, and air lines
- Ducts, housings, impellers, tanks, bottles, and living hinges
- Under-hood and other high-temperature automotive applications
- Jigs, fixtures, and nesting for the shop floor
- Wind tunnel models and end-use parts for aerospace, defense, medical, pharmaceutical, and electronics hardware
SLS or MJF? Both processes build nylon parts in a bed of powder without supports. HP Multi Jet Fusion (MJF) is usually faster and less expensive for small to medium parts, with fine detail and a gray or black finish. SLS is the better choice for larger parts, for a white part that can be dyed or painted, and for glass-filled PA 3200 GF when you need extra stiffness. Not sure which fits? Send us your CAD file and we will recommend one.
SLS 3D Printing Capabilities
| Maximum part size | Up to 27″ × 15″ × 22″ in one piece; larger parts can be printed in sections and bonded |
| Layer thickness | 0.004″ to 0.006″, depending on material |
| Accuracy | ±0.015″ for the first inch, ±0.010″ per inch thereafter (see our part accuracy page) |
| Surface finish | Slightly grainy matte finish; can be dyed, painted, or coated |
| Supports | None needed; parts are supported by the surrounding powder |
| Materials | PA 2200 (PA 12) and PA 3200 GF (glass-filled PA 12) |
Accuracy depends on part size, geometry, and material. SLS builds need time to cool after printing, so plan on at least a couple of days for most jobs; very large parts can take several days to print and cool. Send us your CAD file and we will give you a realistic estimate for your part.
SLS 3D Printing Materials
Each material has its own page with full mechanical properties, data sheets, and part photos.
| Material | Best for |
|---|---|
| PA 2200 (PA 12) | Strong, all-around functional parts; a common substitute for injection-molded nylon. White, biocompatible per EN ISO 10993-1 and USP Class VI (121°C), and suited to moving parts and snap fits. |
| PA 3200 GF (glass-filled PA 12) | Stiff, wear-resistant parts that hold up to heat, such as engine-bay parts and deep-drawing dies. Whitish color with excellent surface quality. |
Key properties at a glance (manufacturer data, X direction):
| Property | PA 2200 | PA 3200 GF |
|---|---|---|
| Tensile strength | 48 MPa | 51 MPa |
| Tensile modulus | 1,700 MPa | 3,200 MPa |
| Elongation at break | 24% | 9% |
| Flexural modulus | 1,500 MPa | 2,900 MPa |
| Shore D hardness | 75 | 80 |
| Heat deflection temp. (0.45 MPa) | — | 157°C (315°F) |
| Melting temperature | 176°C | 176°C |
Finishing Options for SLS Parts
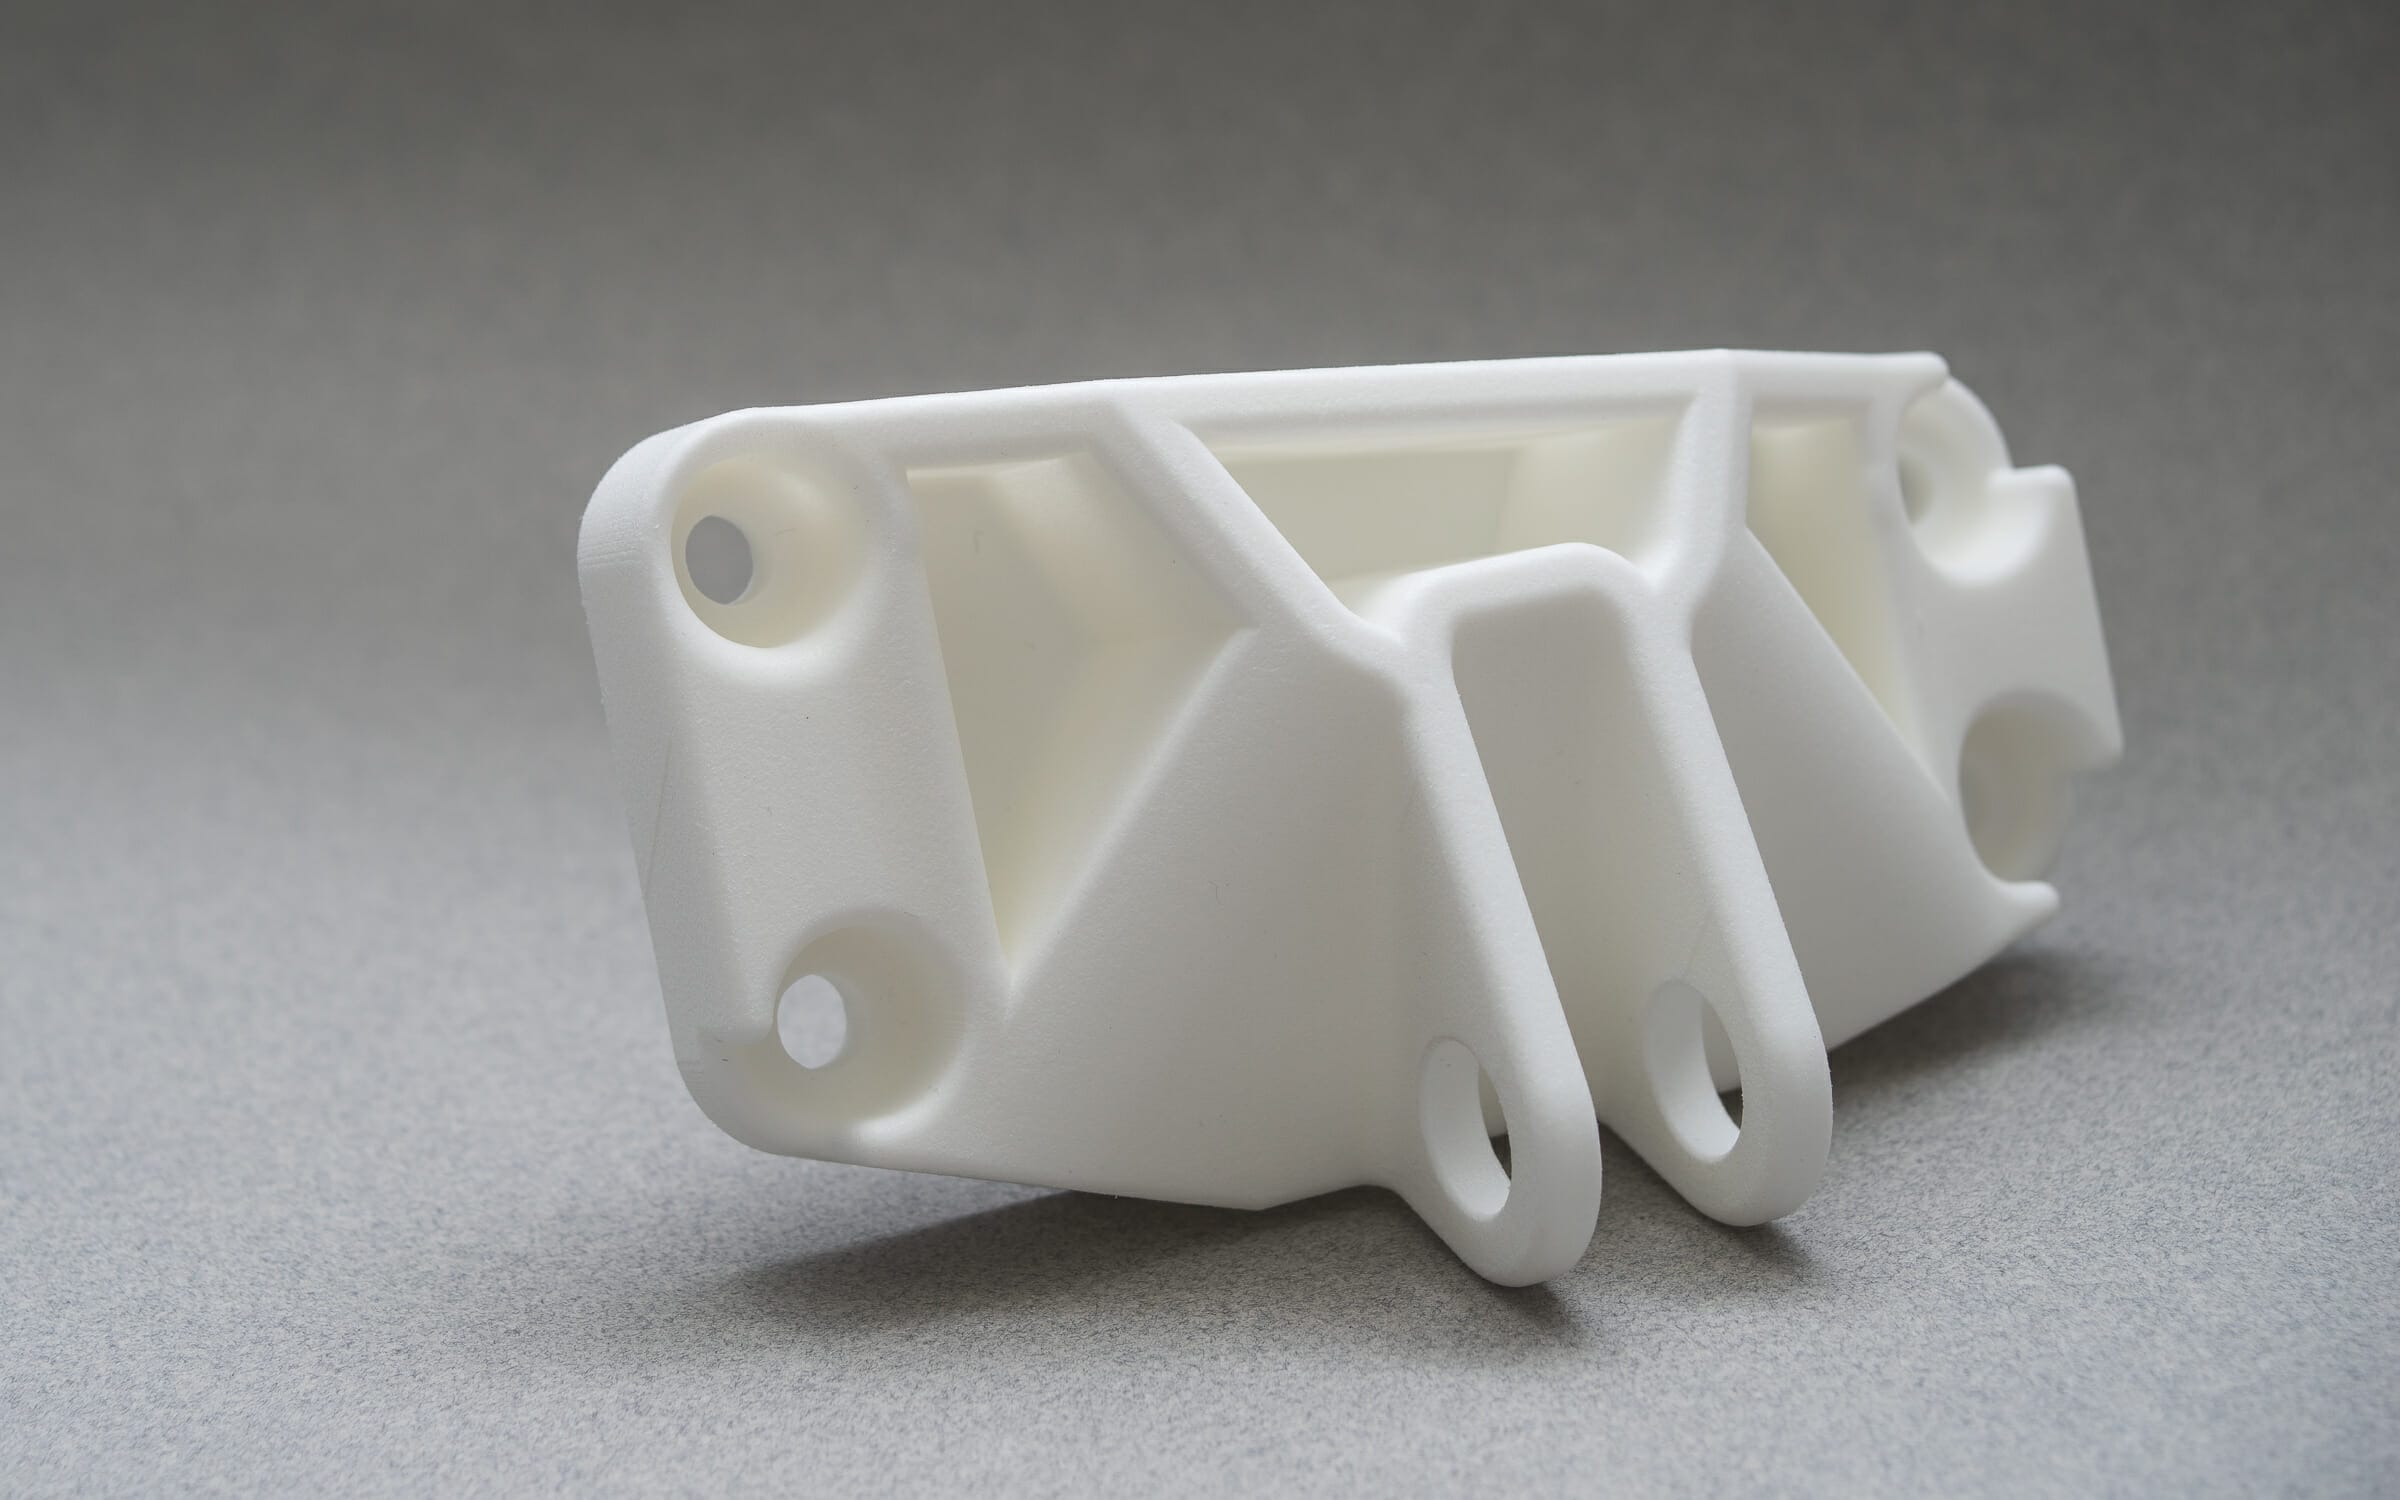
SLS parts come off the printer with a slightly grainy, matte white surface. We can dye, paint (including automotive paint), metal plate, Cerakote, and bond SLS parts. SLS nylon is slightly porous, so parts that need to hold fluid or air should be sealed. See all finishing and post-processing options.
Designing Parts for SLS
Our engineering team at DeWys Engineering designs parts for SLS regularly. If your part isn’t ready to print yet, our design for additive manufacturing services can help, from design review to full CAD design.
If you would rather design the part yourself, these guidelines will help your SLS parts print accurately:
- Keep wall thickness consistent. As with injection molding, consistent walls print more accurately with less warp and twist.
- Add ribs to long, thin parts to reduce the risk of warping.
- Minimum wall thickness: 0.8 mm (0.03″).
- Minimum hole diameter: 1.5 mm (0.06″).
- Minimum feature size (pins and other protruding features): 0.8 mm (0.03″).
- Embossed and engraved details: at least 1 mm (0.04″) deep or tall so they stay visible.
- Text: at least 2 mm (0.08″) tall (about 14 pt); sans serif fonts read best.
- Clearance between mating parts: 0.5 mm (0.02″).
- Overhangs and internal channels need no supports, so you can embed features such as conformal cooling channels or air lines deep inside a part. Leave a way for loose powder to escape.
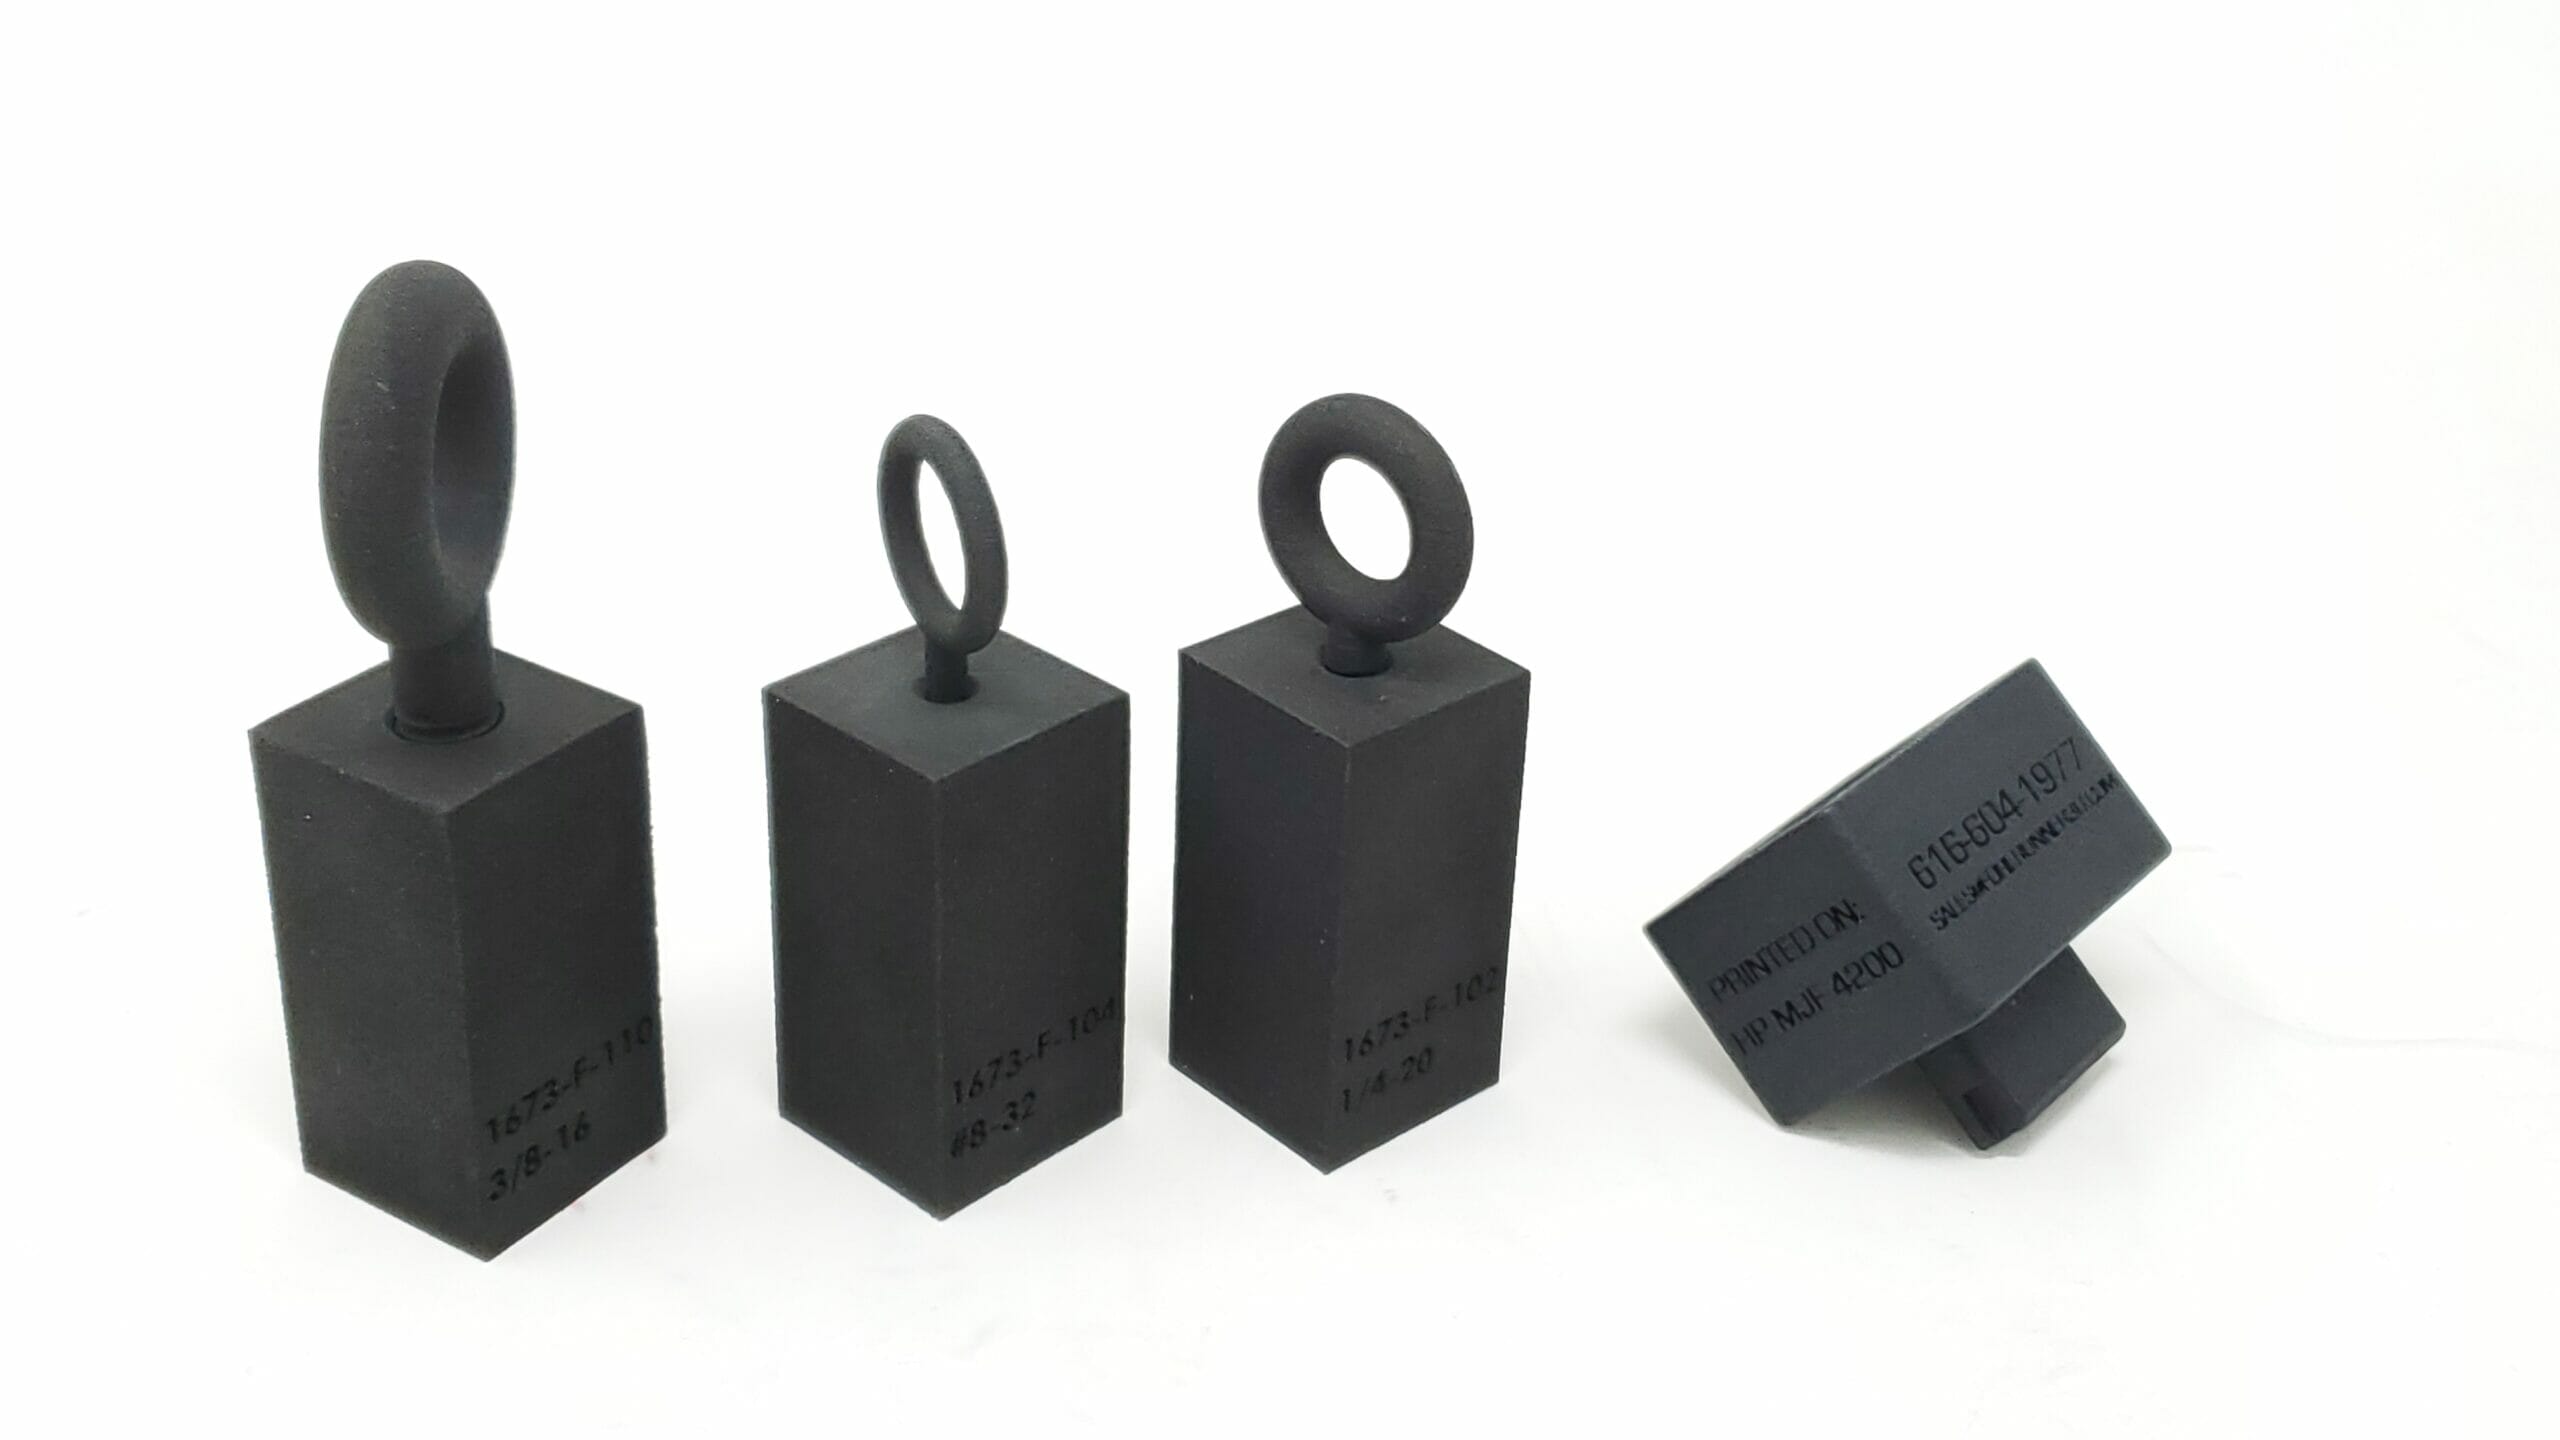
SLS can produce many functional features, including axles, threads, tanks, and hinges. Combined with the strength of engineering nylon, that makes it a common choice for end-use parts.
SLS Part Examples


SLS 3D Printing FAQ
How strong are SLS parts?
SLS nylon parts are strong and durable enough for functional and end-use parts. PA 2200 has a tensile strength of about 48 MPa and is often used in place of injection-molded nylon. PA 3200 GF is nearly twice as stiff, for parts that must hold their shape under load or heat.
How big can SLS parts be?
Up to 27″ × 15″ × 22″ in one piece. Larger parts can be printed in sections and bonded.
Is SLS or MJF better for my part?
Both make strong nylon parts without supports. HP Multi Jet Fusion (MJF) is usually faster and more economical for small to medium parts. SLS is better for larger parts, white parts, and glass-filled nylon. Send us your file and we will recommend the best fit.
How fast can I get SLS parts?
SLS builds have to cool slowly after printing, usually about as long as the print itself, so plan on at least a couple of days for most jobs. Very large parts can take several days to print and cool. We will give you a lead time with your quote.
Are SLS parts watertight?
Not straight off the printer. SLS nylon is slightly porous, so parts that need to hold fluid or air should be sealed after printing.
What colors are SLS parts?
SLS parts print in white. They can be dyed (black is common) or painted to almost any color.
ISO 9001:2015 Certified Quality
Our quality management system is certified to ISO 9001:2015 and covers engineering, additive manufacturing, post-processing, and inspection, so customer requirements are handled consistently from quote to delivery. Learn more about our ISO 9001:2015 certification.