SLS – PA 2200 (PA-12)
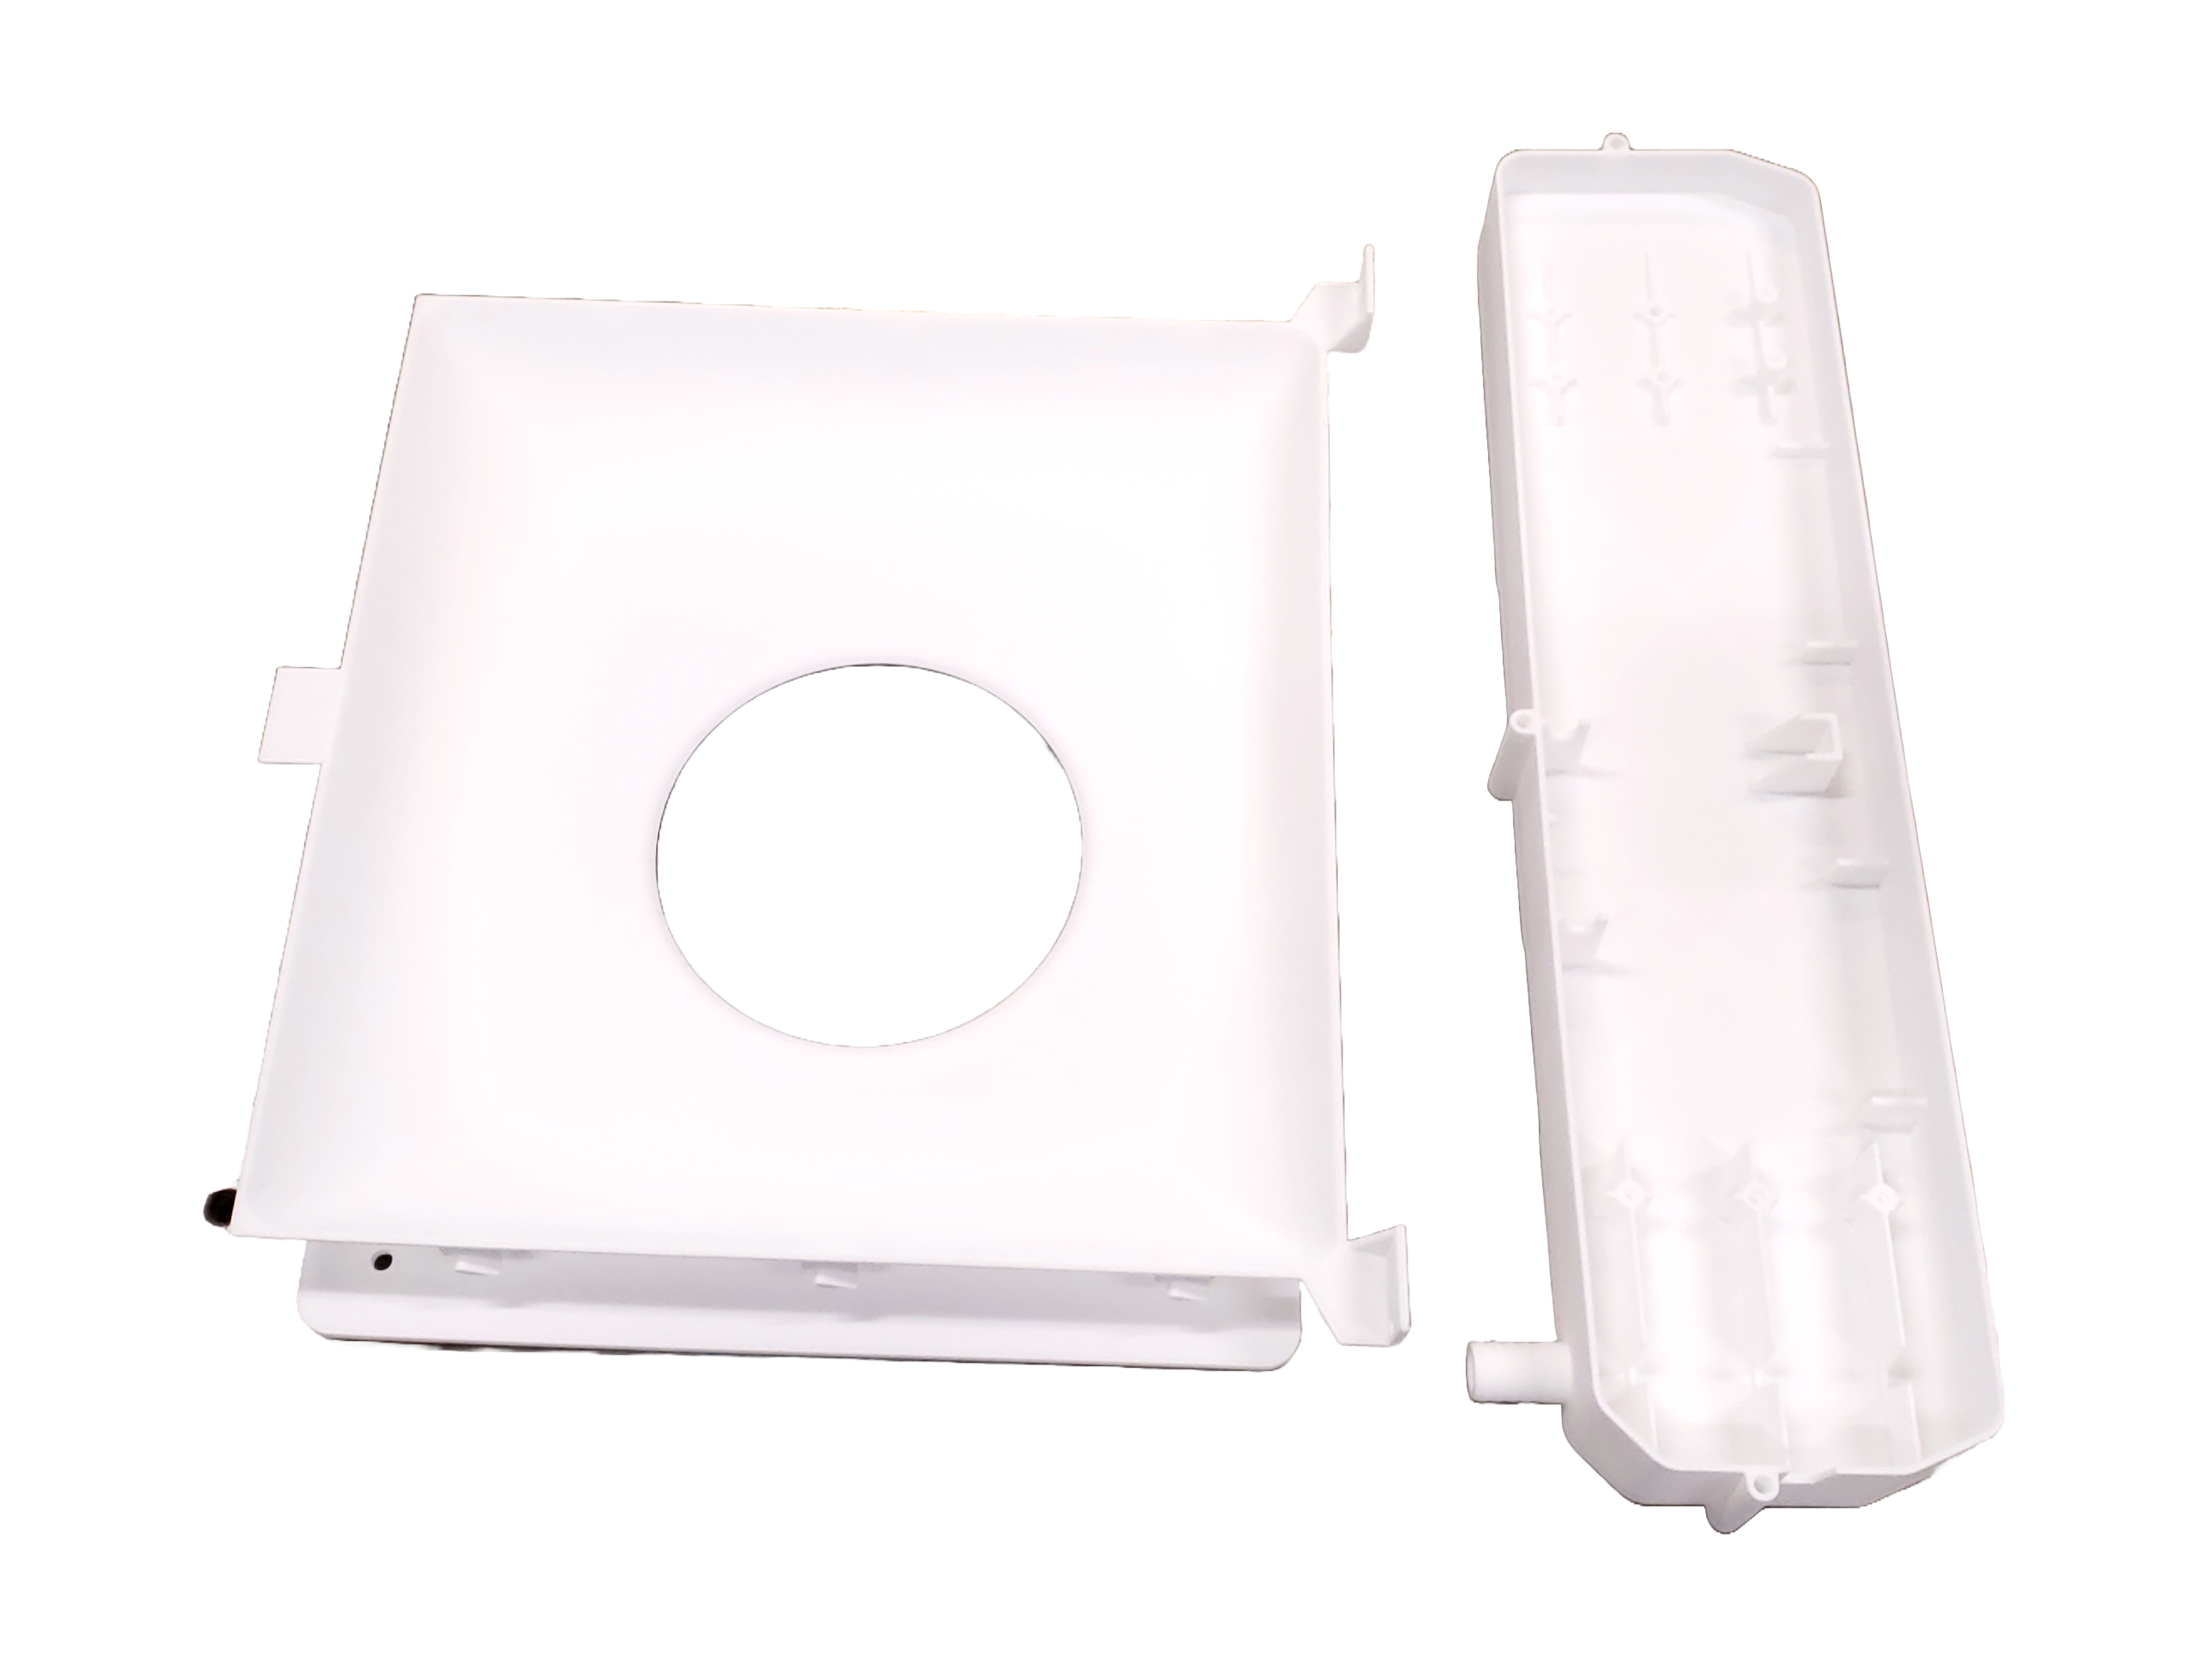
PA 2200 is an unfilled Nylon 12 (PA-12) powder for SLS 3D printing and one of the most widely used SLS materials in the industry. It balances strength, stiffness, and toughness, with good chemical and abrasion resistance, and its mechanical properties make it a common substitute for injection-molded nylon. EOS describes it as the most proven SLS material on the market. Because SLS can build parts up to 27″ × 15″ × 22″ in one piece, PA 2200 is our go-to nylon for larger parts. Parts print in white and can be dyed, painted, or coated.
What PA 2200 Is Best For
- Larger nylon parts that are too big for MJF
- Functional prototypes, including parts with hinges or threads
- Production equipment such as grippers, jigs, and fixtures
- Spare parts such as brackets and covers, including automotive parts
- Production parts and replacements for injection-molded nylon
- Surgical cutting guides and bone models
- Eyewear and other consumer goods
When another material is a better fit
- Smaller nylon parts, or parts you want dyed black as standard: MJF Nylon 12 is usually faster and more economical
- Need more stiffness and heat resistance: PA 3200 GF (glass-filled PA-12)
- Need a flexible, rubber-like part: MJF TPU
Key Material Facts
- Unfilled Nylon 12 (PA-12) with a balanced property profile; white
- Tensile strength: 48 MPa (X/Y), with 18% elongation at break
- Heat deflection temperature: 157°C (315°F) at 0.45 MPa and 64°C (147°F) at 1.80 MPa
- UL 94 HB at 0.5, 1.6, and 3.2 mm
- Compliant with EU food-contact regulation (EC) No. 1935/2004 and GMP, per EOS
- Low coefficient of friction and very good abrasion resistance
- Good chemical resistance
- Layer thickness: 0.004″ to 0.006″
- Maximum part size: 27″ × 15″ × 22″ in one piece; larger parts can be printed in sections and bonded
- Slightly porous; parts that must hold air or fluid should be sealed
Chemical resistance

SLS PA 2200 (PA-12) Material Properties
Mechanical, thermal, and electrical properties (from EOS’s current published data sheet for PA 2200 at 120 µm layers; typical values, dry)
| Property | Value | Test standard |
|---|---|---|
| Tensile modulus, X / Y / Z | 1650 MPa | ISO 527-1/-2 |
| Tensile strength, X / Y | 48 MPa | ISO 527-1/-2 |
| Tensile strength, Z | 42 MPa | ISO 527-1/-2 |
| Strain at break, X / Y | 18% | ISO 527-1/-2 |
| Strain at break, Z | 4% | ISO 527-1/-2 |
| Flexural modulus, X | 1500 MPa | ISO 178 |
| Charpy impact strength (+23°C), X | 53 kJ/m² | ISO 179/1eU |
| Charpy notched impact strength (+23°C), X | 4.8 kJ/m² | ISO 179/1eA |
| Izod notched impact strength (+23°C), X | 4.4 kJ/m² | ISO 180/1A |
| Shore D hardness, X | 75 | ISO 7619-1 |
| Melting temperature | 176°C | ISO 11357-1/-3 |
| Heat deflection temperature (1.80 MPa), X / Z | 64°C / 57°C | ISO 75-1/-2 |
| Heat deflection temperature (0.45 MPa), X / Z | 157°C / 145°C | ISO 75-1/-2 |
| Vicat softening temperature, X | 176°C | ISO 306/B50 |
| Flammability (0.5, 1.6, and 3.2 mm) | HB | UL 94 |
| Comparative tracking index (CTI), X / Y / Z | ≥600 | IEC 60112 |
| Density | 0.93 g/cm³ | EOS method |
More information is available from EOS, the material manufacturer.
Finish and Color Options
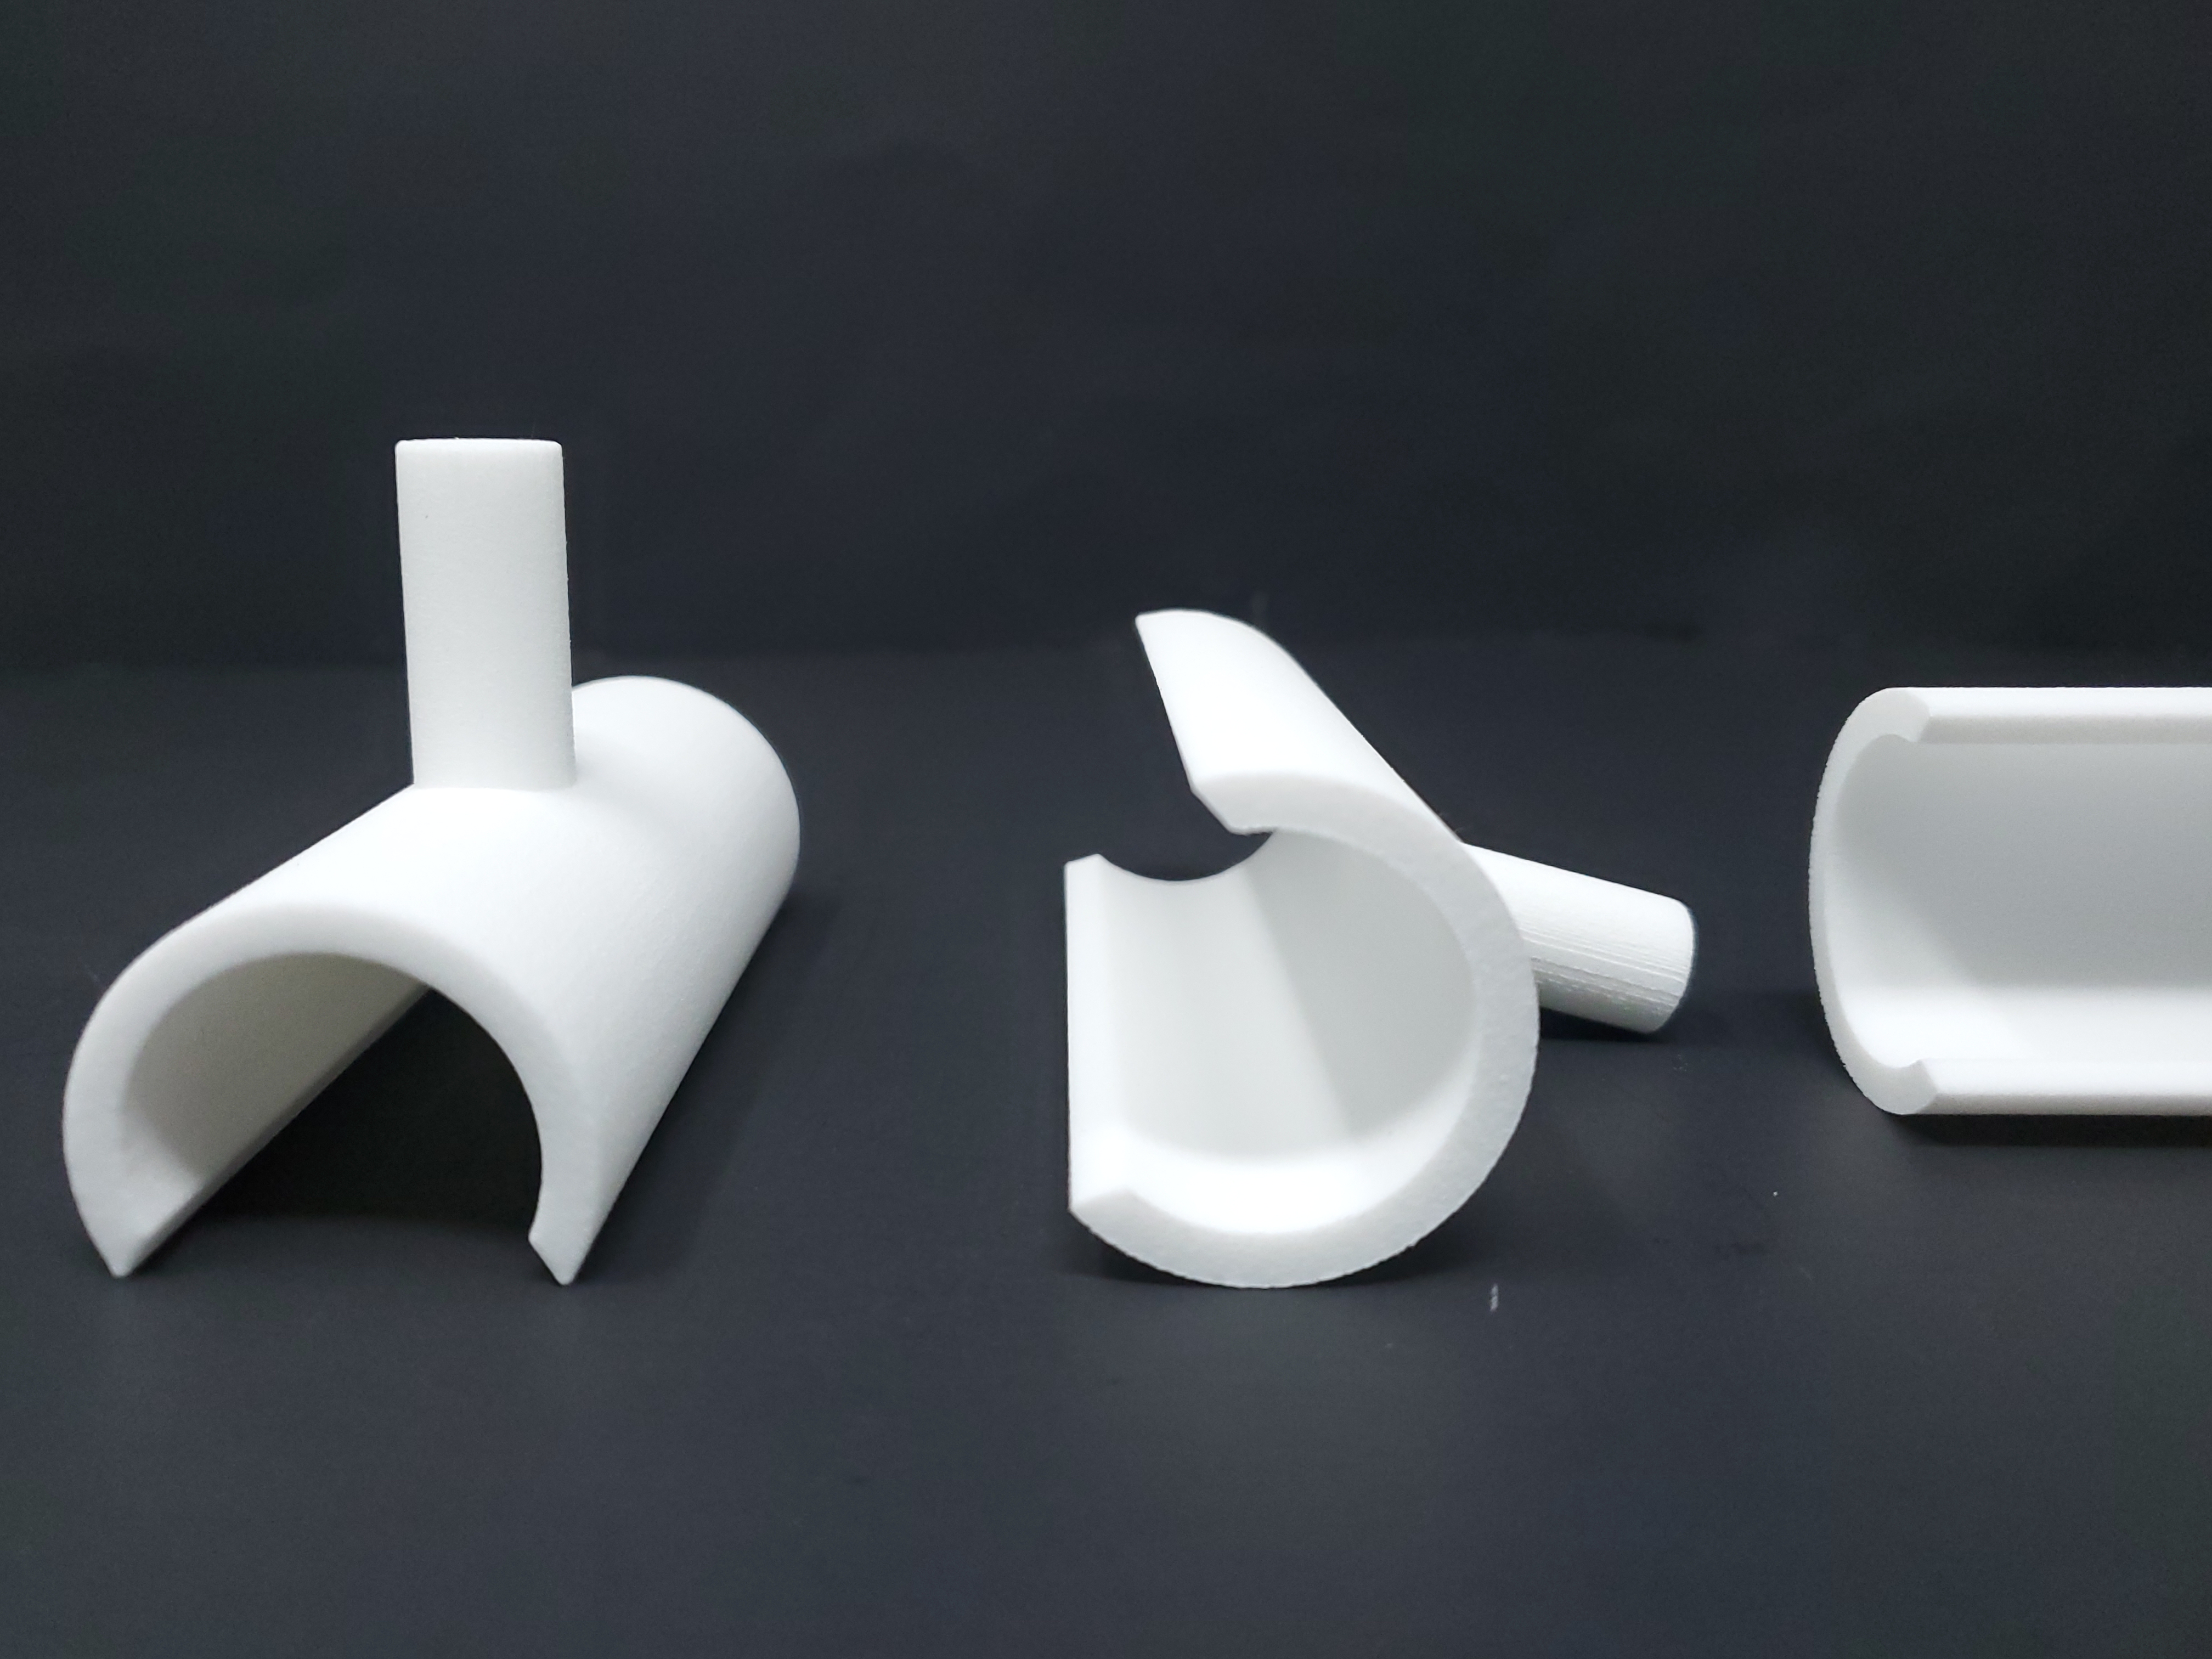
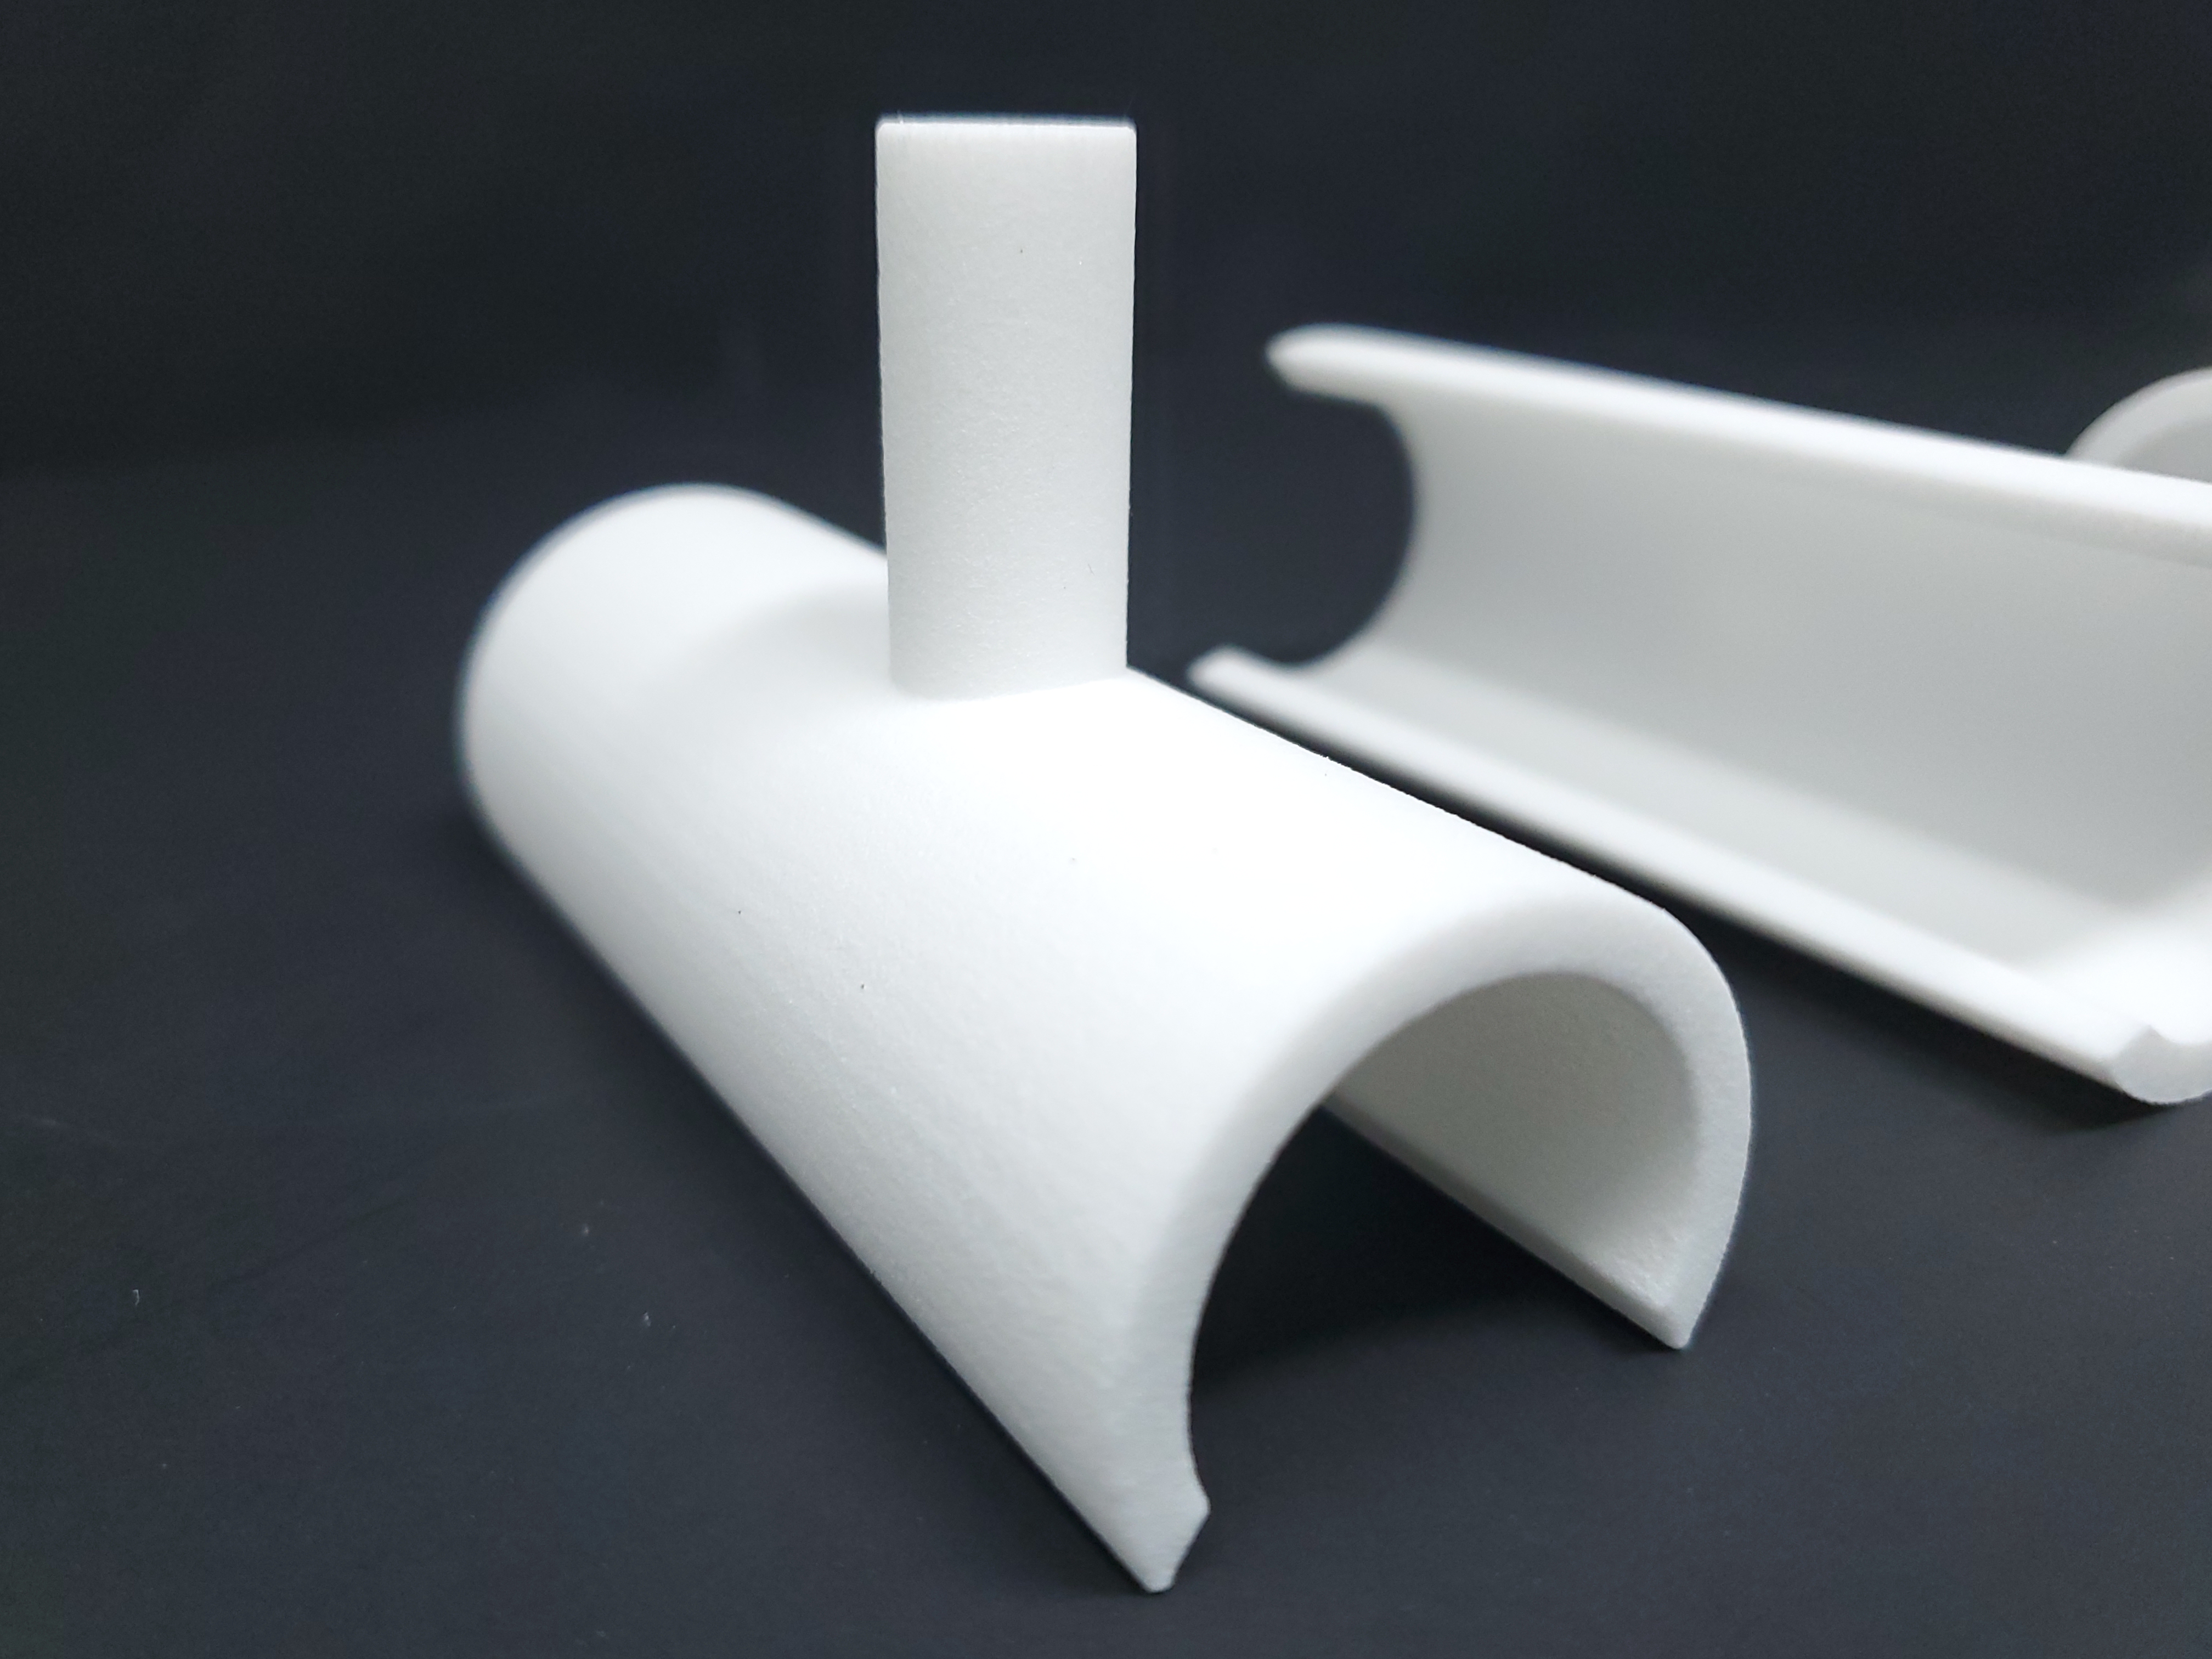
Natural white: parts are cleaned of loose powder and bead blasted, leaving a slightly grainy, matte white surface.
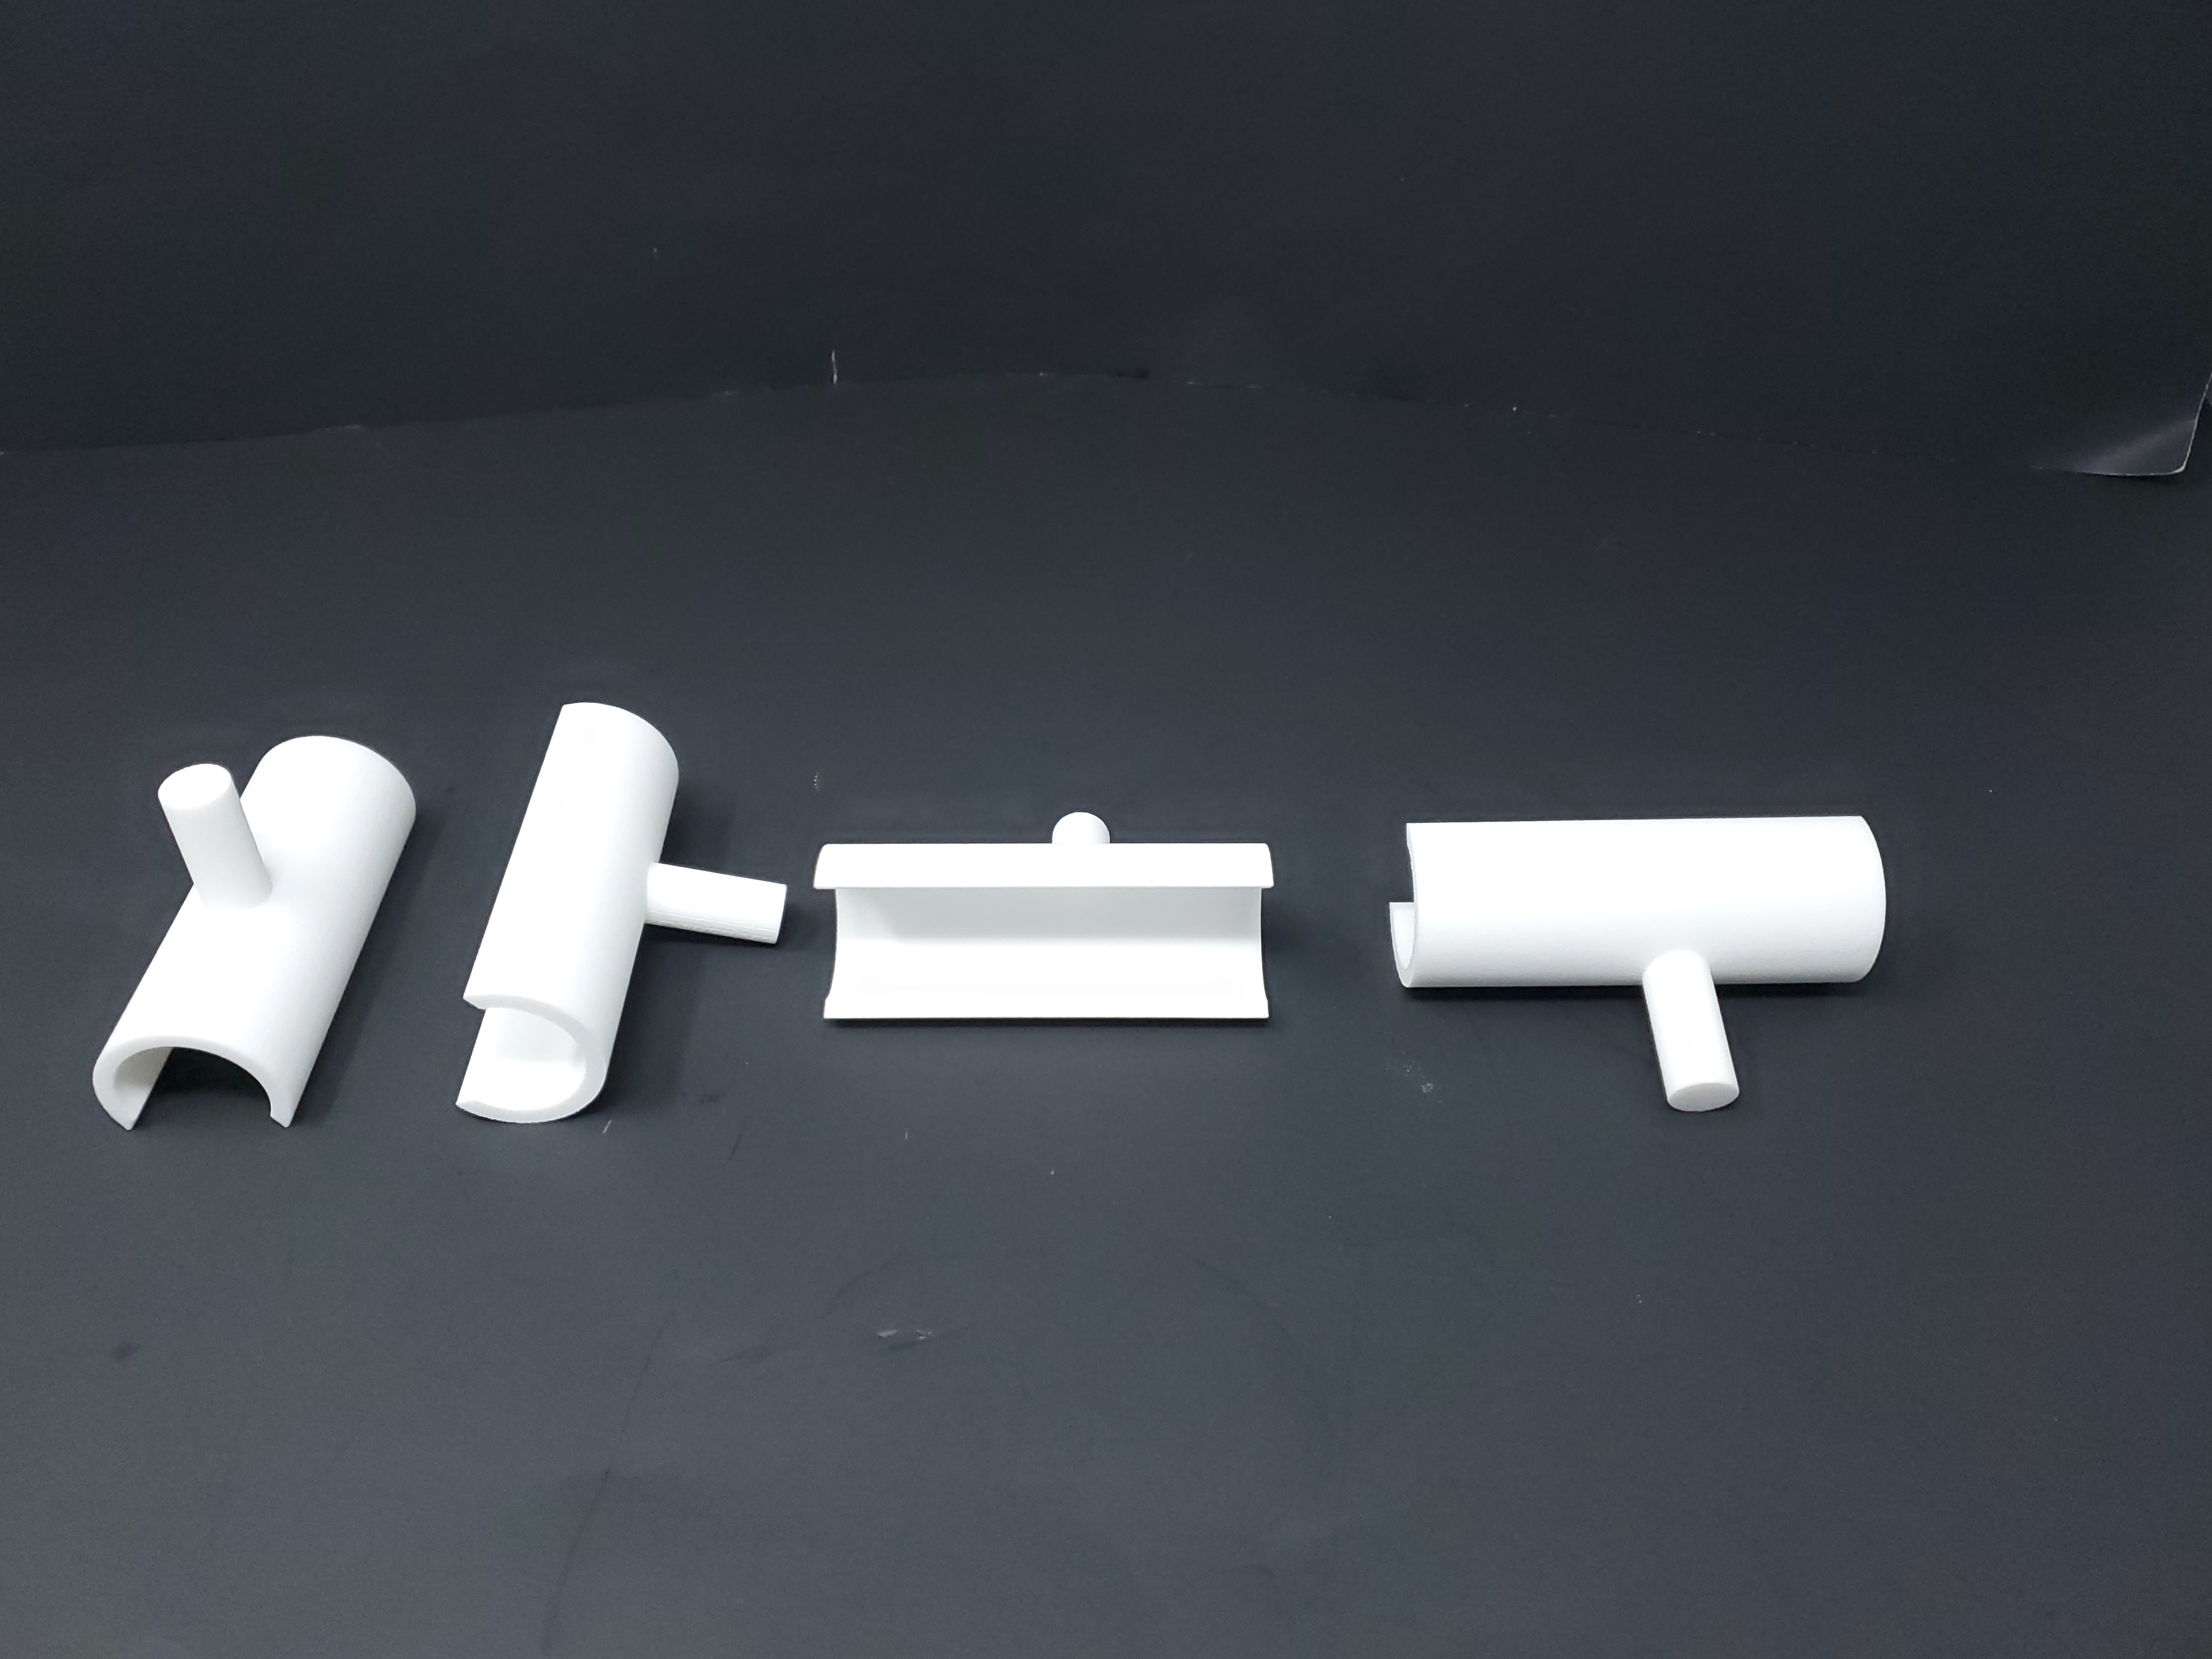
Dyed: PA 2200 parts can be dyed; black is the most common color.

Vapor smoothing: seals and smooths the surface. Vapor smoothing options.
Paint, Cerakote, and plating: PA 2200 parts can be painted (including automotive paint), Cerakoted, or metal plated.
See all of our finishing and post-processing options.
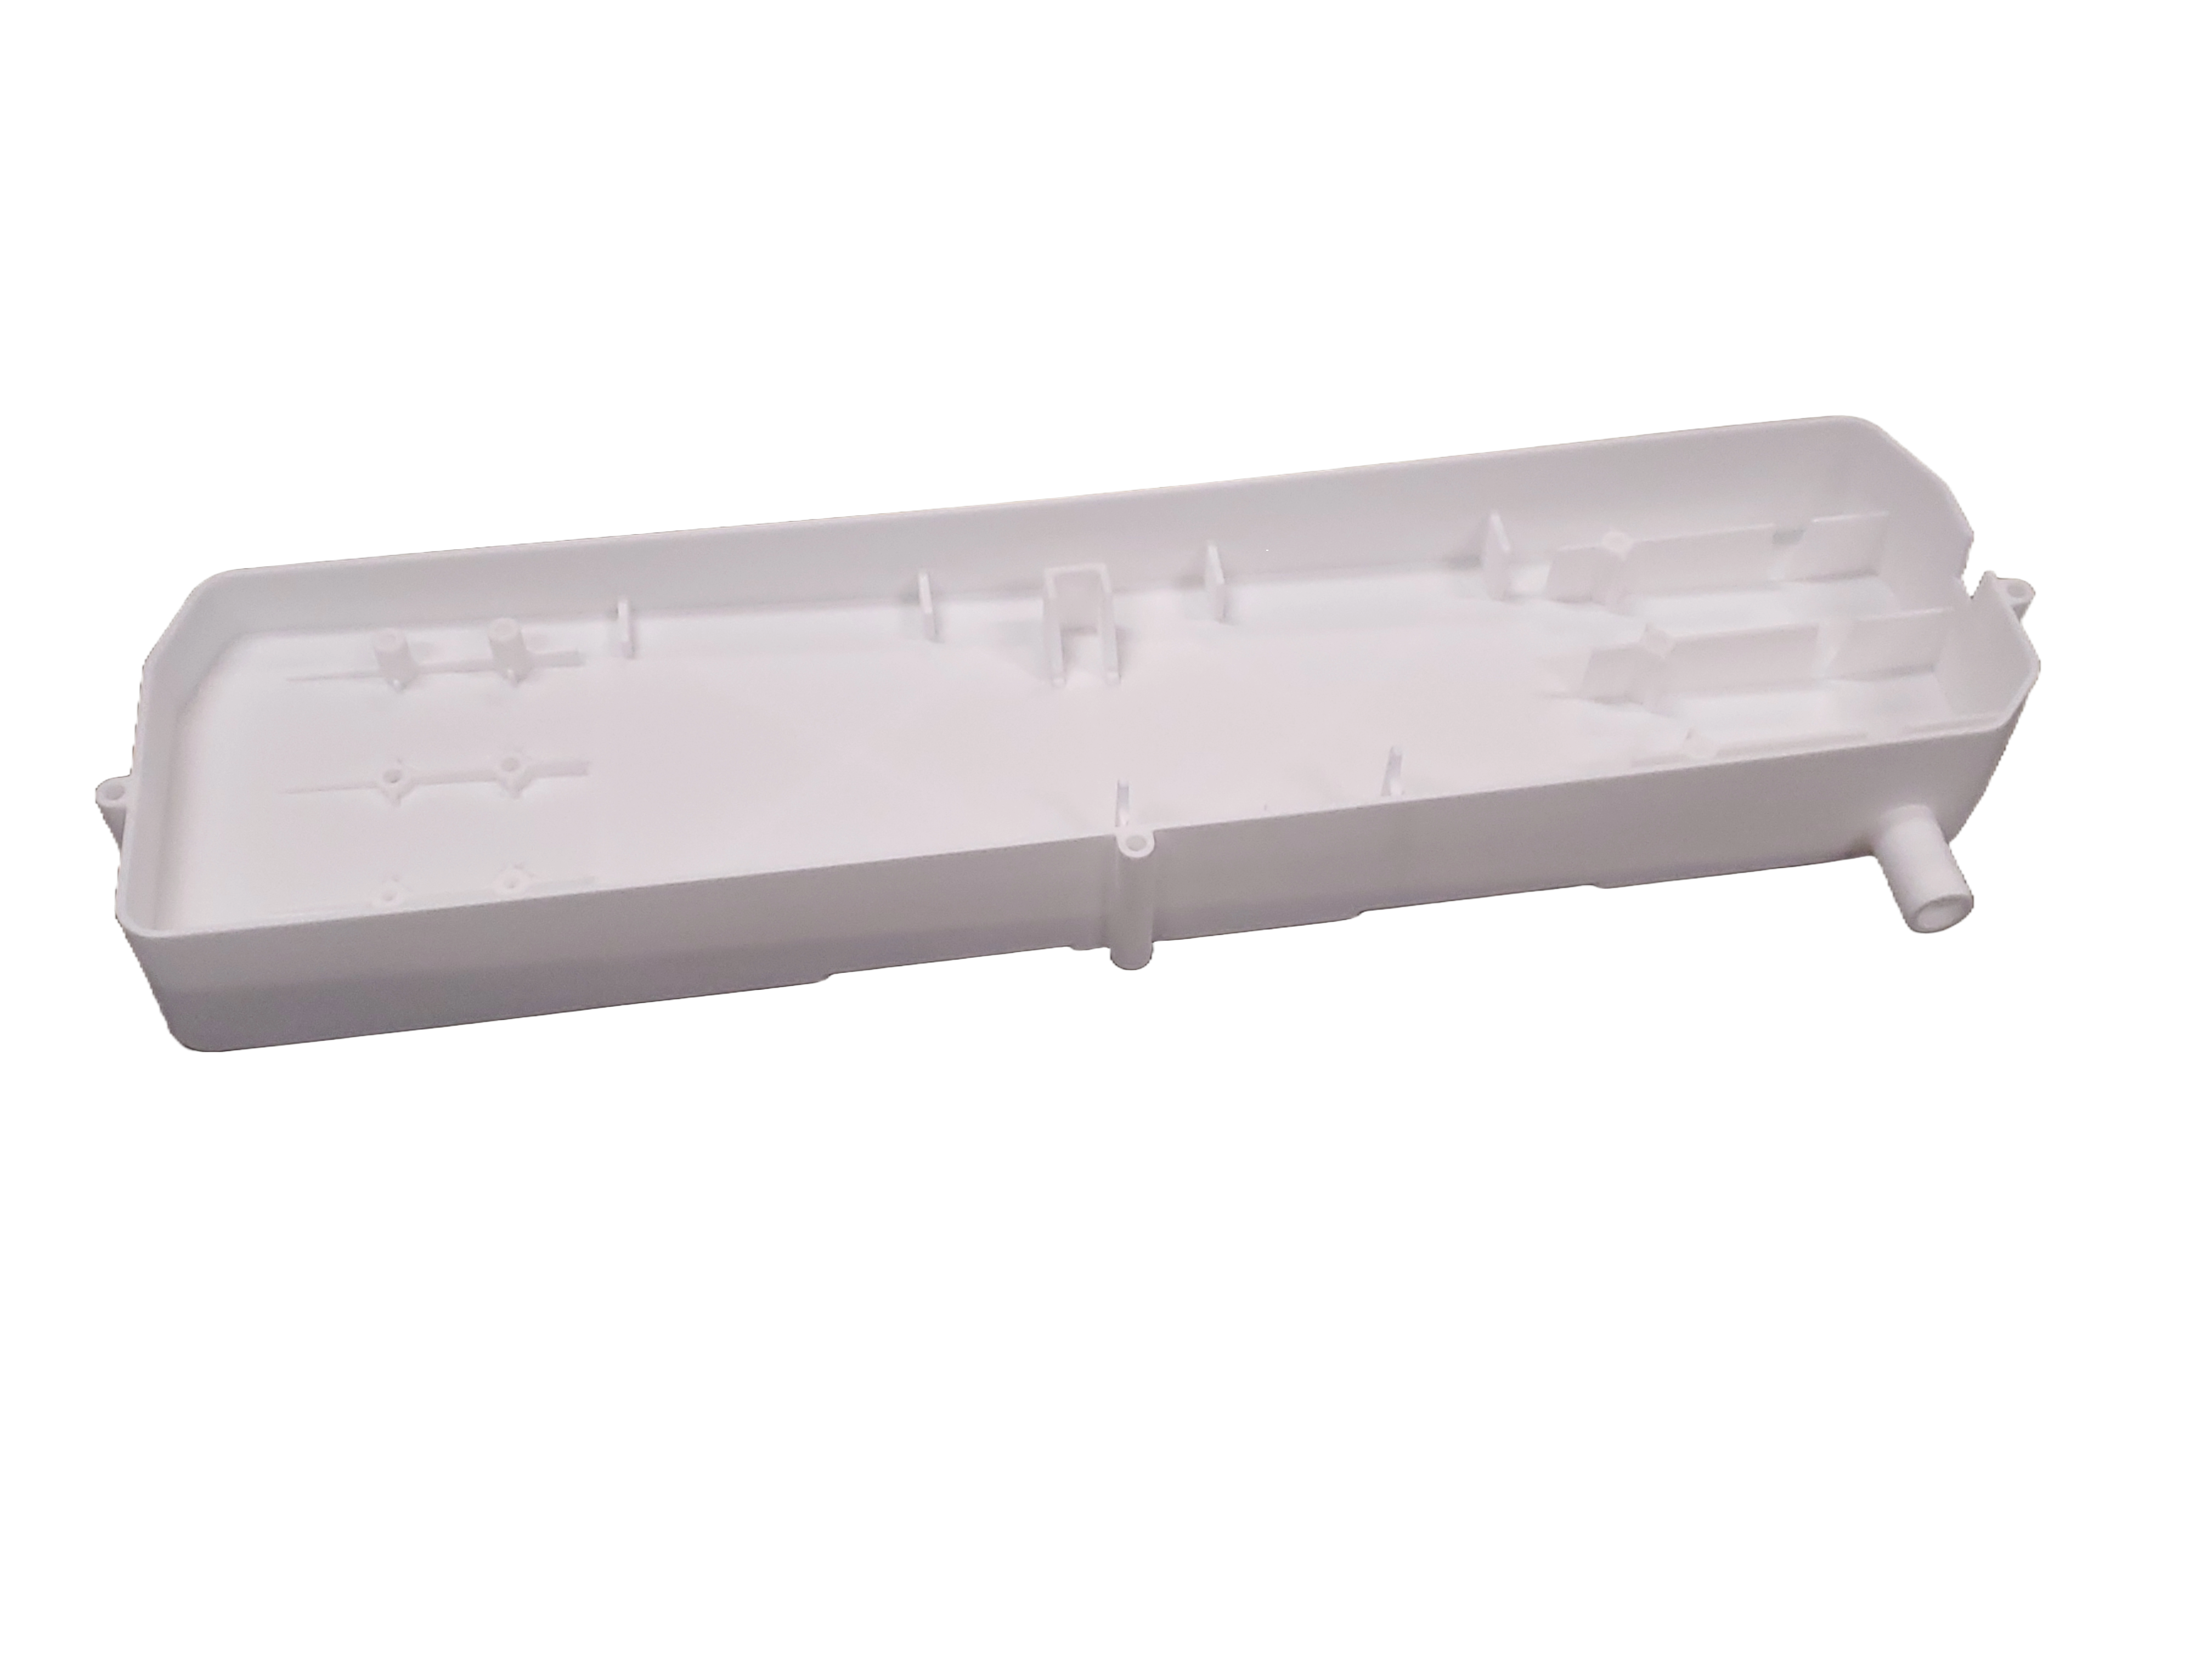
PA 2200 Part Gallery


Related Resources
- SLS 3D printing overview
- Accuracy of 3D printed parts
- Machine and material comparison
- Finishing and post-processing
If you like what you see...
You should sign up for our quarterly email newsletter! We send out a summary of all the latest testing videos, design guides, and anything else cool that has been added to the F3DP website 4 times a year.
We hate spam as much as you do so we only send all killer content and no filler BS!