Nylon 12 (PA-12) – MJF 3D Printing Material
Nylon 12 (PA-12) is the workhorse material for HP Multi Jet Fusion. It is an engineering-grade thermoplastic that produces dense, strong parts with fine detail and consistent mechanical properties in every direction, so it works equally well for functional prototypes and for production end-use parts. Black-dyed PA-12 is our standard MJF finish, at no extra charge.
What Nylon 12 Is Best For
- Functional prototypes that need to perform like the production part
- Low-volume and bridge production with no tooling (see how customers use MJF for production)
- Housings, enclosures, brackets, and connectors
- Fixtures, nests, and end-of-arm tooling
- Snap fits, living hinges, and complex multi-part assemblies
- Parts that must be air or fluid tight
- Lattice structures and lightweighted parts
When another material is a better fit
- Need more stiffness and dimensional stability: PA-12 Glass Beads
- Need a flexible, rubber-like part: TPU M95A
- Need clear parts or a very smooth cosmetic surface straight off the printer: SLA resins
Key Material Facts
- Layer thickness: 0.003″ (0.08 mm)
- Minimum feature size: 0.020″ (0.5 mm)
- Heat deflection temperature: 347°F (175°C) at 66 psi
- Air and fluid tight right off the printer, with no sealing required
- Excellent chemical resistance to oils, greases, aliphatic hydrocarbons, and alkalies (see the full chemical compatibility list)
- Biocompatible: meets USP Class I–VI and US FDA guidance for intact skin surface devices
- Strength and wear testing data from our own MJF parts
Assembly and secondary operations
Nylon 12 machines, drills, and taps much like billet nylon, and it works with the common ways of joining and fastening parts:
MJF Nylon 12 (PA-12) Material Properties
Mechanical properties (from HP’s published data sheet)
| Property Description | Measurement |
|---|---|
| Tensile strength, max load, XY | 48 MPa / 6960 psi |
| Tensile strength, max load, Z | 48 MPa / 6960 psi |
| Tensile modulus, XY | 1700 MPa / 247 ksi |
| Tensile modulus, Z | 1800 MPa / 261 ksi |
| Elongation at break, XY | 20% |
| Elongation at break, Z | 15% |
| Flexural strength (@ 5%), XY | 65 MPa / 9425 psi |
| Flexural strength (@ 5%), Z | 70 MPa / 10150 psi |
| Flexural modulus, XY | 1730 MPa / 251 ksi |
| Flexural modulus, Z | 1730 MPa / 251 ksi |
| Izod impact notched (@ 3.2 mm, 23ºC), XYZ | 3.5 kJ/m2 |
| Heat deflection temperature (@ 0.45 MPa, 66 psi), XY | 175 ºC / 347 ºF |
| Heat deflection temperature (@ 0.45 MPa, 66 psi), Z | 175 ºC / 347 ºF |
| Heat deflection temperature (@ 1.82 MPa, 264 psi), XY | 95 ºC / 203 ºF |
| Heat deflection temperature (@ 1.82 MPa, 264 psi), Z | 106 ºC / 223 ºF |
Material certifications
- USP Class I–VI and FDA Intact Skin Surface Devices guidance for biocompatibility and medical applications
- ISO 10993-5 and ISO 10993-10 tests for in vitro cytotoxicity and skin sensitization
- REACH, RoHS, and PAHs compliant for chemical safety
- UL 94 and UL 746A certification for flame resistance
- UL 94 HB blue card certification for HP PA-12
- Statement of Composition for Toy Applications
Why the UL blue card matters: UL’s blue card identifies the specific processing equipment and settings a material must be produced with to claim compliance. The older yellow card ratings still apply to injection molding and extrusion, but they do not carry over to 3D printing. A filament made from yellow-card pellets, for example, is not UL recognized.
Flammability Testing
We ran the same 5-second flame test on raw, vapor-smoothed, and Cerakote-coated Nylon 12 parts to show how the finish changes the way the part burns.


Finish and Color Options
Raw gray: the part is bead blasted and left in the natural gray color it comes off the printer. More raw gray examples.

Black dye (standard): the part is bead blasted and dyed black. This is our standard finish for MJF Nylon 12 unless you request something else, and there is no extra charge for it. More black dye examples.

Vapor smoothing: seals and smooths the surface for a cleaner look and easier cleaning. Vapor smoothing options.
Cerakote: a thin, durable ceramic coating available in a wide range of colors. Cerakote on 3D printed parts.

Semi-gloss polish: an automated blast polishing process that closes up the grainy bead-blasted texture, so Nylon 12 parts feel smoother, resist scuffing, and take black dye more evenly. Semi-gloss polished finish.
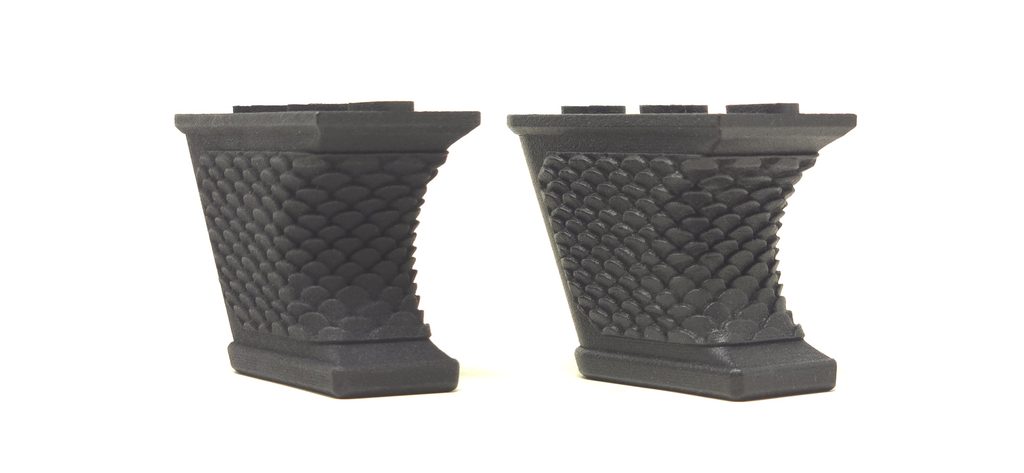
See all of our finishing and post-processing options.
Nylon 12 Part Gallery


Nylon 12 Material Testing Videos
Watch the full rocket testing video.
Related Resources
- How HP Multi Jet Fusion works
- MJF part design guide
- Accuracy of 3D printed parts
- HP Multi Jet Fusion overview
If you like what you see...
You should sign up for our quarterly email newsletter! We send out a summary of all the latest testing videos, design guides, and anything else cool that has been added to the F3DP website 4 times a year.
We hate spam as much as you do so we only send all killer content and no filler BS!