MJF – PA-12 40% Glass Beads (PA-12 GB)
PA-12 Glass Beads (PA-12 GB) is a 40% glass bead-filled Nylon 12 for HP Multi Jet Fusion. The glass beads make parts stiffer, more dimensionally stable, and more heat resistant than standard Nylon 12. The trade-off is much lower elongation at break, so PA-12 GB parts are more brittle and can crack if they are dropped or knocked around. We recommend it when an application specifically calls for its stiffness or heat resistance; for most other parts, Nylon 12 is the tougher choice. Black-dyed PA-12 GB is our standard finish, at no extra charge.
What PA-12 GB Is Best For
- Housings and enclosures that need to stay stiff and hold their shape
- Prototypes that simulate glass-filled injection-molded parts, including their snap features
- Higher-temperature applications that need a higher heat deflection temperature than standard Nylon 12
- Parts where dimensional stability matters more than impact resistance
- Production parts, when the application really needs the stiffness or heat resistance
When another material is a better fit
- Fixtures, jigs, tooling, and parts that will get dropped or knocked around: Nylon 12 (PA-12). Its much higher elongation makes it far more forgiving.
- Snap fits and living hinges on general-purpose parts: Nylon 12 (PA-12)
- Need a flexible, rubber-like part: TPU M95A
- Need a larger glass-filled part: SLS PA 3200 GF
Key Material Facts
- 40% glass bead filled Nylon 12
- Tensile modulus up to 2,700 MPa (392 ksi), about 50% stiffer than standard Nylon 12
- Heat deflection temperature: 347°F (175°C) at 66 psi and up to 248°F (120°C) at 264 psi
- Layer thickness: 0.003″ (0.08 mm)
- Minimum feature size: 0.020″ (0.5 mm)
- Air and fluid tight right off the printer, with no sealing required
- Excellent chemical resistance to oils, greases, aliphatic hydrocarbons, and alkalies (see the full chemical compatibility list)
- Elongation at break of about 10%, versus 15–20% for standard Nylon 12, so parts are more brittle; snap features work but are more fragile
Assembly and secondary operations
PA-12 GB works with the common ways of joining and fastening parts:
MJF PA-12 GB Material Properties
Mechanical and thermal properties (from HP’s published data sheet; typical values)
| Property Description | Measurement |
|---|---|
| Tensile strength, max load, XY | 30 MPa / 4351 psi |
| Tensile strength, max load, Z | 30 MPa / 4351 psi |
| Tensile modulus, XY | 2500 MPa / 363 ksi |
| Tensile modulus, Z | 2700 MPa / 392 ksi |
| Elongation at break, XY | 10% |
| Elongation at break, Z | 10% |
| Flexural strength (@ 5%), XY | 57.5 MPa / 8340 psi |
| Flexural strength (@ 5%), Z | 65 MPa / 9427 psi |
| Flexural modulus, XY | 2400 MPa / 348 ksi |
| Flexural modulus, Z | 2700 MPa / 392 ksi |
| Izod impact notched (@ 3.2 mm, 23ºC), XYZ | 3 kJ/m2 |
| Shore D hardness | 82 |
| Heat deflection temperature (@ 0.45 MPa, 66 psi), XY | 174 ºC / 345 ºF |
| Heat deflection temperature (@ 0.45 MPa, 66 psi), Z | 175 ºC / 347 ºF |
| Heat deflection temperature (@ 1.82 MPa, 264 psi), XY | 114 ºC / 237 ºF |
| Heat deflection temperature (@ 1.82 MPa, 264 psi), Z | 120 ºC / 248 ºF |
| Part density | 1.3 g/cm³ / 0.047 lb/in³ |
Material certifications
- UL 94 HB blue card certification for HP PA-12 GB
- Summary of regulatory compliance and environmental attributes
Why the UL blue card matters: UL’s blue card identifies the specific processing equipment and settings a material must be produced with to claim compliance. The older yellow card ratings still apply to injection molding and extrusion, but they do not carry over to 3D printing. A filament made from yellow-card pellets, for example, is not UL recognized.
Finish and Color Options
Raw gray: the part is bead blasted and left in the natural gray color it comes off the printer. More raw gray examples.

Black dye (standard): the part is bead blasted and dyed black. This is our standard finish for MJF PA-12 GB unless you request something else, and there is no extra charge for it. More black dye examples.

Vapor smoothing: seals and smooths the surface for a cleaner look and easier cleaning. Vapor smoothing options.
Cerakote: a thin, durable ceramic coating available in a wide range of colors. Cerakote on 3D printed parts.

Semi-gloss polish: an automated blast polishing process that closes up the grainy bead-blasted texture, so PA-12 GB parts feel smoother, resist scuffing, and take black dye more evenly. Semi-gloss polished finish.
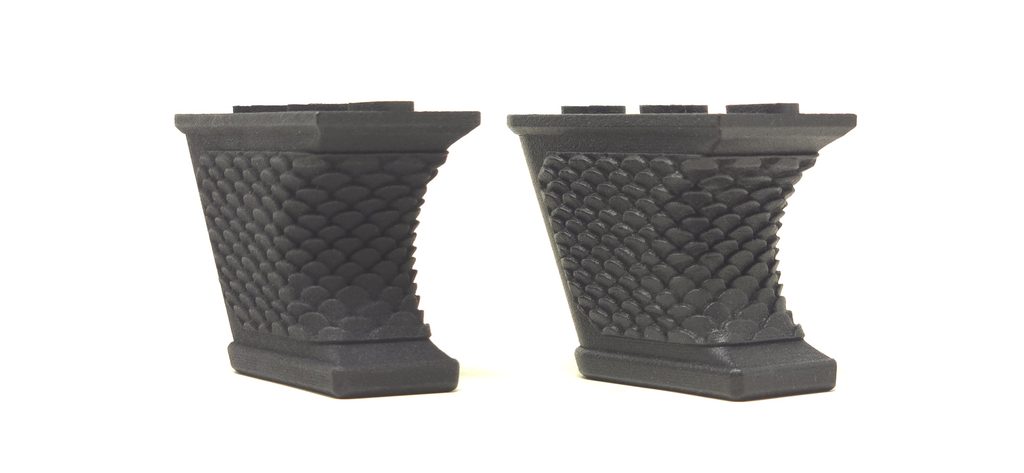
See all of our finishing and post-processing options.
PA-12 GB Part Gallery


PA-12 GB Material Testing Videos
Watch the full rocket testing video.
Related Resources
- How HP Multi Jet Fusion works
- MJF part design guide
- Accuracy of 3D printed parts
- HP Multi Jet Fusion overview
If you like what you see...
You should sign up for our quarterly email newsletter! We send out a summary of all the latest testing videos, design guides, and anything else cool that has been added to the F3DP website 4 times a year.
We hate spam as much as you do so we only send all killer content and no filler BS!